

Why weld a housing instead of casting it
Gearbox housings used to be cast, and plenty still are. But when a customer needs one unit or five, and needs them in six weeks instead of six months, welded fabrication is the practical answer. We have built replacement housings for gearboxes where the original casting was discontinued twenty years ago.
The trade-off is discipline in the build. A welded housing only works if the bearing seats end up in the right place after welding, so we machine after final welding, never before.
Welded construction also lets you change things mid-project. A customer wanted an extra inspection cover and an oil level sight glass added after the first sample was built. On a casting that would mean a new pattern and another month. On a welded housing it meant cutting two holes and welding on two bosses, done in an afternoon.
How we build it
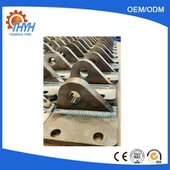
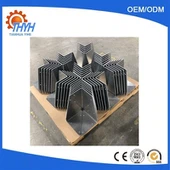
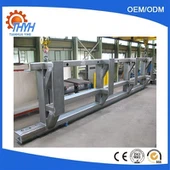
Plate comes in Q235, Q345 or Q355 depending on the loads you give us. We cut on plasma or laser, tack the shell, then run the long seams with a set welding sequence that keeps distortion down. Internal ribs go in where the drawing calls for them.
After welding, the mounting faces and bearing bores get machined in one setup. Bearing seats are held to H7 unless you specify tighter. That single-setup step is what keeps the input and output shafts parallel.
The welding sequence itself is written to pull the shell evenly. We weld the side seams first, then the top and bottom, alternating sides so the heat balance stays symmetrical. On housings over 800 mm long we add a temporary bracing frame inside to stop the shell from bowing during welding, and cut it off after stress relief.
What goes wrong when you skip steps
The classic mistake is machining the bearing seats before welding. The weld heat moves the steel a few tenths of a millimeter, and the seats are now out of position. The gearbox goes together, runs for a week, and the bearings start singing because the shafts are no longer parallel.
Another one is leaving the internal ribs out because the customer thinks they are optional. They are not optional if the housing carries radial loads. Without them the side walls deflect under load and the gear mesh opens up.
We have fixed both of these on housings that came to us from other shops. The repair is usually: cut the welds open, add the ribs that should have been there, re-weld, stress relieve, re-machine. It costs more than doing it right the first time.
Product attributes
| Material | Q235B / Q345B / Q355B carbon steel |
|---|---|
| Plate thickness | 6 to 50 mm, per drawing |
| Bearing seat tolerance | H7 standard, tighter on request |
| Welding | ISO 3834 qualified, balanced sequence, internal bracing on long units |
| Machining | Faces and bearing bores in one setup after welding |
| Stress relief | Vibration aging or annealing on units over 800 mm |
| Finish | Shot blasted to Sa2.5, anti-rust primer coating |
| Inspection | Dimensional report, bore concentricity, weld visual, material certificate |
| Certificates | ISO 9001, ISO 3834, AWS D1.1 welders |
| Lead time | Samples 15 to 20 days, batch 30 to 45 days |
Frequently asked questions
Can you match the footprint of an existing gearbox housing?
Yes. Send us the old housing or a sketch with the bolt pattern and bearing locations. We do not need the original drawing, just the dimensions that matter: foot bolt centers, shaft center height, bearing OD, and the overall envelope. We have built replacements for gearboxes where the maker went out of business decades ago.
Why not just cast it?
For one-off or small batch work, casting means a pattern, a foundry slot, and a longer lead time. Welded fabrication is faster and you can modify the design between units without re-tooling. For quantities above 200 units a year the economics flip and casting becomes worth the pattern cost. We can advise on the break-even if you are deciding.
Do you machine the housing or do I need to find a machine shop?
We machine it. Bearing seats, mounting faces, seal grooves and thread holes all come out of our shop ready to bolt up. You receive a finished part with a dimensional report, not a welded blank.
What tolerance can you hold on the bearing bore?
H7 is standard, which is plus a few hundredths on nominal. If your bearing needs a tighter interference fit we can hold H6 or K6 on the bore. The limiting factor is wall thickness around the seat, so we will tell you if the plate is too thin for a tight tolerance.
How do you handle distortion during welding?
The weld sequence is written to pull the shell evenly, we tack rigidly before the long seams, and on longer units we use internal bracing that comes out after stress relief. After welding we measure the shell and record the as-welded dimensions before machining, so we know exactly how much material we are removing.
Working with us
We are a 7,000 square meter fabrication shop in Qingdao with 20 years of export experience, mostly to Australia. Welding runs under ISO 3834 with welders qualified to AWS D1.1, and quality is documented to ISO 9001 from material certificate to final dimensional report. Drawings and specifications stay confidential. Send us the drawing, even a marked-up photo of the old housing. We quote within 24 hours.
Hot Tags: custom welded gearbox housing frame | q235 q345 q355 carbon steel, iso 9001 oem, China custom welded gearbox housing frame | q235 q345 q355 carbon steel, iso 9001 oem manufacturers, suppliers, factory